ERM2030 CNC Router for Large-Format Wood Cutting and Carving
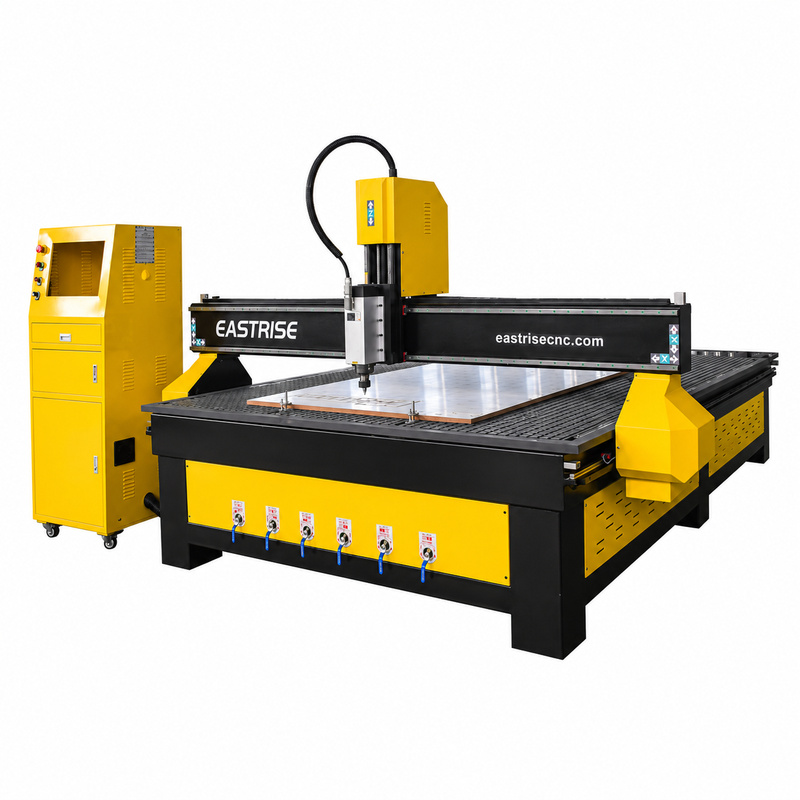
Large-Format Routing for Woodworking Projects
The Eastrise ERM2030 combines a 2000 × 3000 mm working area with 3-axis motion for cutting, engraving and carving. It supports woodworking applications ranging from panel components to decorative work.
A larger table gives workshops more freedom to arrange parts, but usable sheet coverage still depends on fixtures, tool clearance and the cutting layout. Check your actual sheet dimensions before selecting a machine.
Machine Features and Configuration
Spindle and tooling: The published spindle options are 3, 4.5 and 5.5 kW. Choose tooling for the material, finish and depth of cut rather than selecting spindle power alone.
Linear motion and maintenance: Guide surfaces, drive components and lubrication points need regular inspection. Keep chips away from moving components and follow the maintenance schedule supplied with the machine.
Electrical cabinet: Provide suitable access for qualified maintenance personnel. Confirm the electrical supply and controller requirements for the quoted configuration.
Vacuum workholding: Check the sealing condition of the sheet and spoilboard before cutting. Small parts may need a different holding strategy from a full panel; plan the last cutting passes so parts remain secure.
MDF Cabinet Doors and Furniture Panels
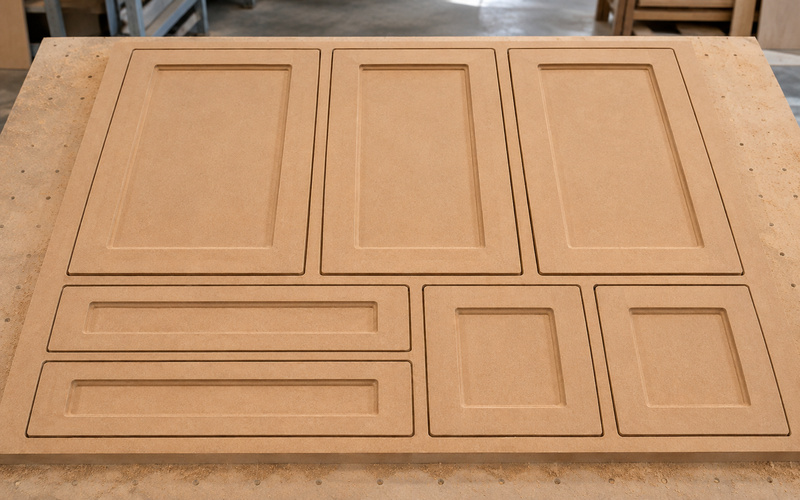
Routing can produce recessed profiles, pockets and shaped outlines in MDF components. Plan the operation sequence around the surface finish required after machining.
For painted doors, assess routed edges as well as the flat face. A suitable cutter, stable workholding and a finishing allowance can reduce the amount of preparation needed before coating. Approve a representative sample before processing a batch.
Plywood Components and Speaker Enclosures
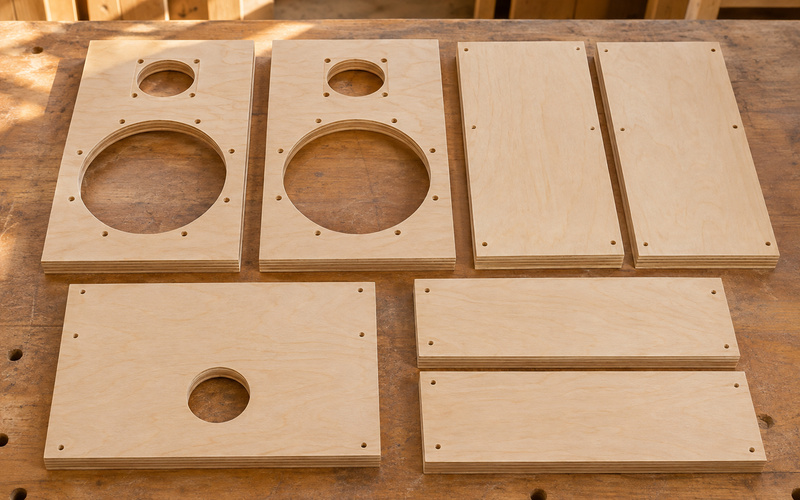
Plywood projects often combine external profiles, circular openings and assembly holes. Keeping these features in one referenced setup helps their positions remain consistent.
Match the cutter geometry to the face finish required. Inspect both sides of a sample because a clean upper surface does not guarantee a clean lower edge. Confirm that the smallest parts remain held throughout the toolpath.
Solid Wood Relief Carving and Decorative Panels
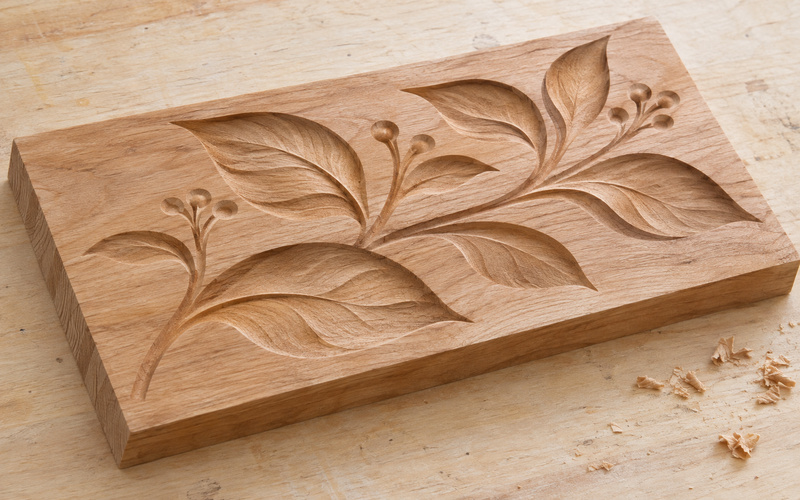
Three-axis relief carving works well for shapes accessible from above. Use a roughing operation to remove bulk material, followed by a suitable finishing toolpath to refine visible surfaces.
Grain direction, tool condition and finishing stepover influence the result. Test delicate details before machining the full panel, and allow for sanding where the design requires it. Undercuts need a different setup or machining approach.
ERM2030 Technical Specifications
| Parameter | Specification |
| Model | ERM2030 |
| Working area | 2000 × 3000 mm |
| Published maximum feeding height | 200 mm; customization listed |
| Maximum travel speed | 30,000 mm/min |
| Spindle power options | 3 / 4.5 / 5.5 kW |
| Spindle speed range | 6000–24,000 rpm |
| Voltage options | 220 / 380 V; confirm supply requirements |
Travel speed is a positioning specification, not a guaranteed cutting feed rate. Feeding height is not the thickness that can be cut in one pass. Tool length, fixtures, spindle position and material behavior determine the practical machining limits.
Confirm the final controller, drive arrangement, table, utilities and supplied accessories in the quotation.
A Practical CAD-to-Part Workflow
Prepare the part geometry and check dimensions.
Select the material, cutter and workholding method.
Generate toolpaths in CAM software and use a postprocessor matched to the controller.
Verify tool clearance, work origin and the machining sequence.
Machine a sample and inspect its fit and finish before starting the batch.
A drawing file and a machine-ready program serve different purposes. Confirm the software workflow with your supplier instead of assuming that a controller can machine every drawing format directly.
Frequently Asked Questions
What does 2030 mean?
For this model, it identifies the nominal 2000 × 3000 mm working area.
Does the machine include automatic tool changing?
Do not assume automatic tool changing is included. Confirm tool-change arrangements in the quoted machine configuration.
How should I compare prices?
Compare quotations with the same controller, spindle, workholding equipment, extraction provisions, accessories and support scope. Ask what is included in installation and training.
What information helps prepare a quotation?
Provide your materials, sheet dimensions, typical part files, required finish, expected output and available utilities. A sample machining trial is useful when appearance or assembly fit is critical.

 English